Explore the complete industrial guide to low-temperature drying systems for nutraceuticals, probiotics, and botanical extracts. Learn how Refractance Window, vacuum tray, low-temp spray, freeze, heat pump, thin-film, and vibratory fluid bed dryers preserve active bio-compounds, protect delicate product colors, and maximize thermal efficiency while ensuring full GMP and FDA compliance.
Tag
Modern Industrial Drying Machine Solutions for North East India’s Manufacturing Sectors
An in-depth engineering guide to industrial drying machines, thermodynamic fundamentals, and specialized moisture removal technologies—including Refractance Window Dryers, Spray Dryers, VFBDs, and Paddle Dryers—engineered for food, chemical, agricultural, and waste-to-value processing industries.
Modern Industrial Drying Machine Solutions for North India’s Manufacturing Sectors
An in-depth engineering guide to industrial drying machines, thermodynamic fundamentals, and specialized moisture removal technologies—including Refractance Window Dryers, Spray Dryers, VFBDs, and Paddle Dryers—engineered for food, chemical, agricultural, and waste-to-value processing industries.
Biomass Dryer Machine Manufacturer in India: Advanced Technical Guide to Industrial Drying Systems
Discover high-efficiency industrial biomass drying systems engineered by Genex Tech Industries LLP. From continuous mesh belt and rotary drum dryers to advanced combination fluid bed systems, explore turnkey thermal dehydration solutions designed for pellet production, briquetting, and bioenergy plants worldwide.
GTI Attending as Visitor – Foodpro 2026 (CII Foodpro / 16th Edition) | Genex Tech Industries LLP
Genex Tech Industries LLP (GTI) announces its participation as a trade visitor at CII Foodpro 2026 (16th Edition) from 7–9 August 2026 at the Chennai Trade Centre. Discover how GTI’s ISO 9001:2015 certified industrial dryers, continuous belt dehydration systems, spray dryers, and turnkey food processing solutions drive operational efficiency and sustainable waste-to-value processing across global markets.
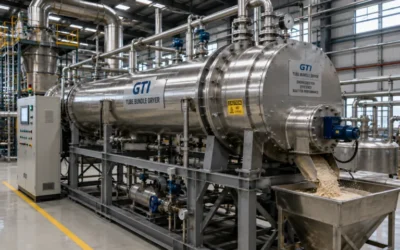
Mastering Industrial Dehydration: The Engineering & Economic Power of Tube Bundle Dryers by Genex Tech Industries
Explore the engineering and economic benefits of industrial Tube Bundle Dryers engineered by Genex Tech Industries. Designed for high thermal efficiency and gentle handling of granular and fibrous materials, this continuous indirect drying technology minimizes energy consumption and reduces dust emissions. Learn how Food Tech Projects acts as your all-in-one solution provider to deliver complete turnkey drying systems for agro-processing, starch extraction, animal feed, distilleries, and biomass recycling.
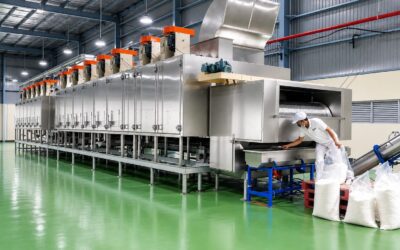
The Ultimate Continuous Band Dryer All-In-One Solution Guide
Explore high-efficiency continuous band dryer systems engineered for food, chemical, and coconut processing. Discover multi-zone thermal airflow technology, technical specs, and industrial applications designed to maximize dehydration yield.
Optimizing Industrial Mineral Dehydration: The Complete Guide to Gypsum, Silica Sand & Calcium Carbonate Drying Systems
Discover advanced thermal dehydration solutions for bulk industrial minerals. Learn how custom-engineered rotary drum, flash, and combination drying systems optimize moisture control, reduce fuel consumption, and maximize throughput for gypsum, silica sand, and calcium carbonate processing lines.
Advanced Thermal Dehydration Engineering: A Technical Deep Dive into Industrial Mesh Belt and Rotary Drum Dryers
An in-depth technical guide comparing Multi-Zone Mesh Belt Dryers and Heavy-Duty Rotary Drum Dryers. Learn how GTI’s advanced thermal dehydration technology optimizes moisture reduction, heat transfer efficiency, and continuous throughput across agro-food, chemical, biomass, and mineral industries.
Engineering Excellence in Coconut Milk Processing: Technical Architecture of GTI Turnkey Systems
Discover GTI’s engineering architecture for turnkey coconut milk processing plants and industrial spray dryers. Learn how twin-screw extraction, high-pressure homogenization, and advanced atomization deliver maximum yields, extended shelf life, and international compliance.